Where designs fail—and what that costs
Most failures start with a drawing that looks right on screen but falls apart under the cutter: tiny fillets where the tool can’t reach, thin walls that vibrate, tolerances tighter than the process can hold. When a part leaves the CAD model and meets the machine, the mismatch creates scrap, rework, and schedule slips. That gap is why teams brief their suppliers early; a reliable precision parts manufacturer will catch impossible features before expensive prototypes are machined.
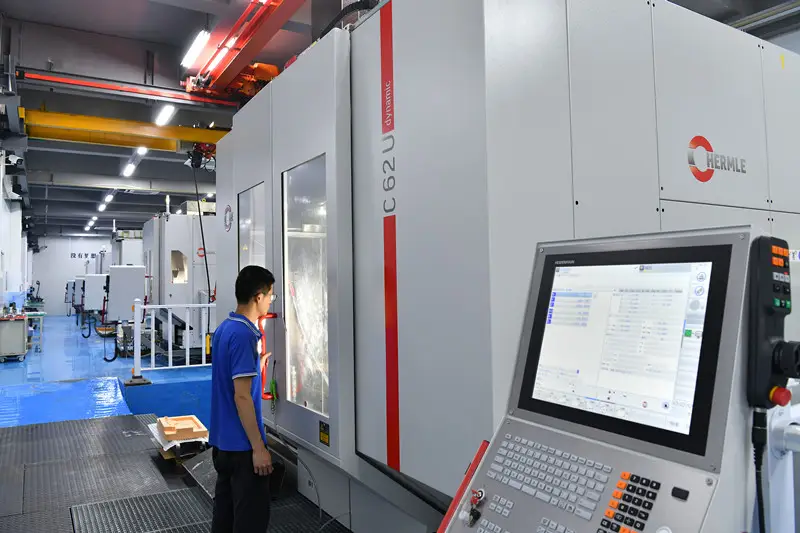
Problem-driven checklist for engineers
Treat each feature as a manufacturing problem. Ask: can a standard end mill access pockets without custom tooling? Are wall thicknesses above 0.8–1.0 mm for aluminum and 1.5–2.0 mm for steels unless supported? Do threads sit far enough from edges to avoid breakout? Specify tolerances only where function demands them—tight tolerances increase cycle time and inspection cost exponentially. Label datum references clearly so shops know which surfaces govern alignment. These checks cut iteration cycles.

What buyers must demand before quotes
Buyers should supply an annotated drawing set: identify critical dimensions, note non-critical cosmetic surfaces, and include expected volumes and delivery windows. Ask suppliers for suggested tooling limitations and a first-off inspection report. Require material certification when form, fit, or fatigue matters. Compare bids on total landed cost—not just price per piece—to include scrappage, secondary ops, and fixture time.
Trade-offs and viable alternatives
When a feature is too costly, pivot to a simpler geometry that preserves function. Replace a deep blind pocket with a through-hole and a counterbore where possible. Consider split assemblies instead of aggressive thin webs. For fine detail that CNC struggles with, evaluate EDM or additive-to-subtractive workflows. Each alternative carries new constraints—EDM adds lead time and upcharges; additive parts often need post-machining for precision faces. Choose the method that aligns with scale, surface finish, and mechanical requirements.
Common mistakes that trigger delays
Don’t lock 3D models without allowing supplier review. Avoid universal tight tolerances; they force slower feeds and lower tool life. Forgetting to call out surface finish results in shops guessing and reworking. Expecting a single supplier to excel equally at low-volume prototypes, tight-tolerance aerospace work, and high-volume automotive stamping is unrealistic—match supplier capability to the job.
Experience, credibility, and a real-world anchor
Decades of shop-floor runs teach what textbooks don’t: cutter access dictates form as much as function, and inspection planning must happen before the first setup. That practical knowledge shows up at events like the International Manufacturing Technology Show in Chicago, where suppliers and OEMs validate techniques and tooling advancements. When you need prototype validation or quick design-for-manufacture feedback, consider tested partners offering cnc prototyping services that include first-article inspection and material traceability. Clear records, sample parts, and traceable processes are the signals of a trustworthy supplier.
How to act on this guidance
Start with a short manufacturability review: send one representative drawing, list critical functions, and invite supplier flags. Use the supplier’s feedback to pare unnecessary tolerances and rework challenging features into machinable forms. For buyers, demand inspection data with first lots. For engineers, lock only the dimensions that matter to performance. These steps reduce iterations and keep costs predictable.
Final synthesis
Design decisions must solve machining problems, not create them. Tighten what matters, simplify what doesn’t, and vet suppliers on concrete deliverables—first-off reports, tooling limits, and material certificates. That practical discipline produces repeatable parts on time; it’s the kind of reliable process you find when a team partners with Hanstar for precision work.