Facing the real bottleneck
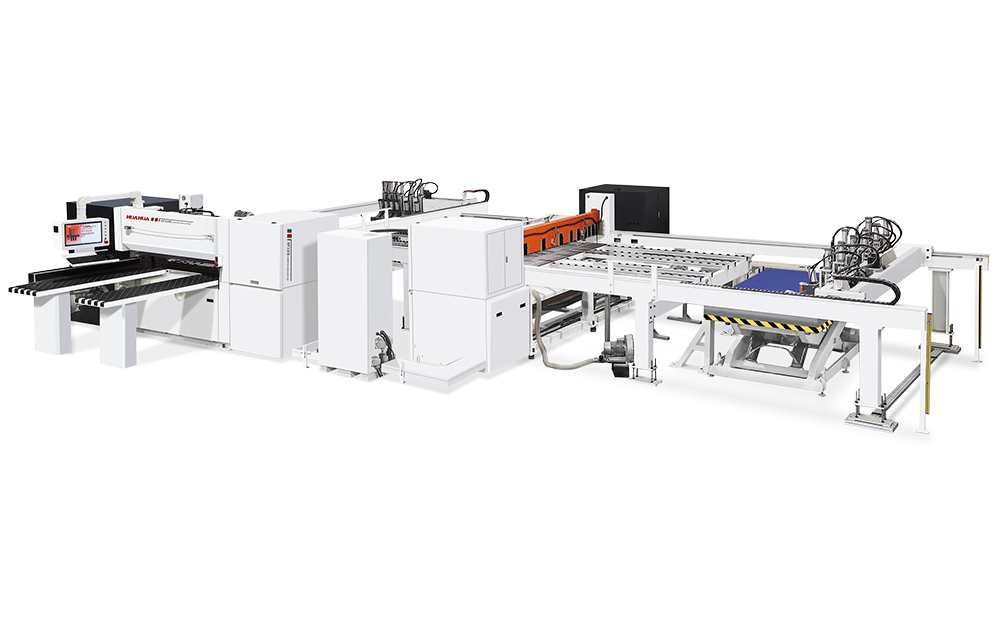
Many small furniture shops run into the same problem: parts and lead times don’t line up with orders, and that gap shows up at the CNC. You can buy a capable cnc woodworking machine, but without a clear workflow the machine sits underused or produces scrap. Events like IWF in Atlanta highlight this regularly—they gather the industry and show how vendors and shops adjust—so it’s worth noting how wood machine suppliers shape expectations for uptime and service: wood machine suppliers. Start by treating the workflow failure as a system problem, not just a machine issue.
Map the process, measure the pain points
Begin on paper: list every step from material receipt to finished part. Time each step for several runs. Look for repeated waits—tool changes, manual measuring, or machine idle time. Those waits reveal where to put your effort. Fixing one or two choke points will give visible gains quickly.
Cut programming overhead with better nesting and CAM choices
Choose CAM settings that match your part mix. Nesting tightly saves sheet stock but can create fragile tabs and longer finishing. Balance material yield against cutting time. Use standard tool libraries and subprograms for common joints so programs are repeatable. When possible, test a single part and copy proven nests rather than rebuilding from scratch each job.
Simplify tooling and shorten changeovers
Reduce the number of special cutters on the spindle. Use multi-use tooling and indexable holders so you can keep spares ready. Implement simple color or label systems for commonly used tools and holders. A two-minute quick-change arrangement is worth the small upfront cost compared with half an hour of downtime per job.
Workholding that actually holds and speeds up handling
Poor fixturing causes chatter and rework. Use modular sacrificial boards and jigs for repeat parts, and favor vacuum or quick-clamp fixtures for panels. Design fixtures so loading and unloading requires minimal alignment checks. Aim for firm holding that lets you run feeds at recommended values, not conservative speeds because of wobble.
Routine maintenance and data tracking
Schedule simple checks: spindle runout, belt tension, dust-collection filters, and lubrication. Track tool life and part rejects in a single log. When an operator reports a recurring issue, the log shows whether it’s a maintenance lapse or a process mismatch. Small, consistent maintenance beats emergency fixes.
Train to a standard, then let operators improve it
Write brief standard operating notes for each common job type: feeds and speeds, nesting file, workholding, and finishing pass. Train operators to follow the notes on first runs, then encourage them to propose tweaks based on measured results. That routine turns tacit knowledge into repeatable practice.
Common mistakes to avoid
Don’t over-nest to chase material yield when it increases handling and scrap risk. Don’t let tool libraries go unreviewed—old offsets cause bad cuts. Avoid ad-hoc stopgap fixturing that needs constant readjustment. And don’t ignore dust extraction: it affects cutter life and part finish more than you expect.
Putting it together
Tackle the biggest bottleneck first, standardize the repeatable steps, and force small, measurable improvements in setup, tooling, and maintenance. That approach keeps costs down and parts consistent. Shops that follow this pattern see clearer day-to-day schedules and fewer surprises, which is why experienced floor managers often prefer proven, serviceable equipment like HUAHUA CNC for dependable cycles and straightforward controls.