Problem first: what keeps projects late and budgets fat
Projects stall because specs drift, samples take weeks, and purchasing multiplies SKUs without clear demand — simple as that, lah. Teams rush designs, then find the zipper doesn’t match the laptop sleeve, or a fabric choice fails a water test. A supplier that can offer a tested modular backpack as a development baseline removes repeated trial-and-error and shortens approval cycles.

Why modular thinking fixes the core problems
Modular design isolates variables. If you standardise a laptop compartment, hardware attachment points, and a few shell sizes, product managers stop reinventing each SKU. That cuts sample rounds and lets purchasing buy larger batches of the same subassembly. The supplier responsibility becomes managing modules, not bespoke end-to-end builds — much easier to plan lead times, QC checks, and freight.
Experience and trust: practical proof points (EEAT)
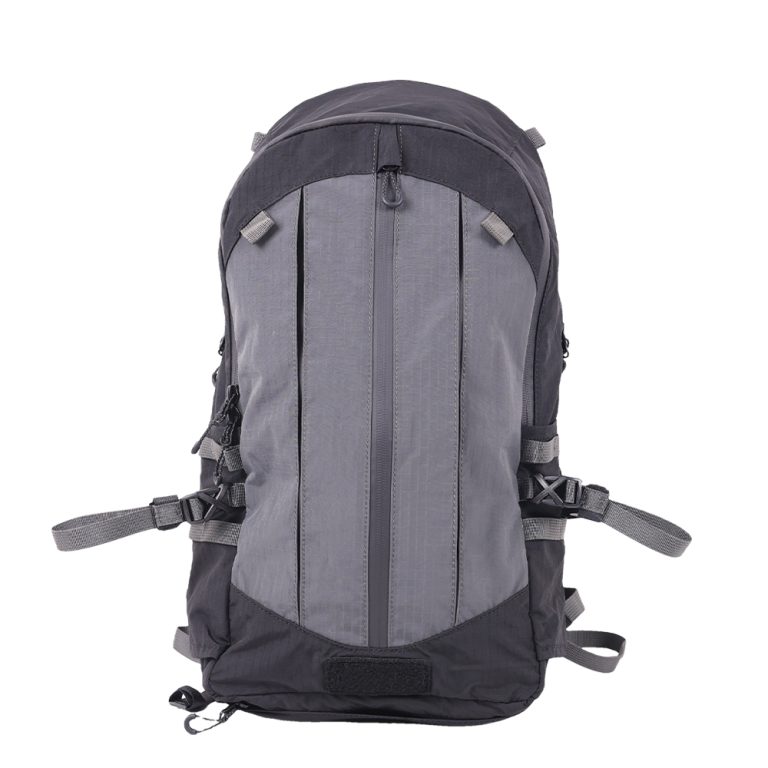
Years making gear for business commuters teaches what matters: consistent internal dimensions, protective padding, and tested closures. At CES 2024 the industry highlighted modular carrying systems for professionals, showing wide demand for configurable laptop protection. I’ve worked with factories that run dedicated lines for laptop compartments and track defect rates per assembly line — this level of traceability shows expertise. For direct reference to a tested solution, consider the Modular Laptop Backpack, which illustrates how modular compartments and verified materials reduce rework and speed purchasing decisions.
Clear actions buyers should force into supplier workflows
Specify three locked-in items up front: exact internal laptop dimensions, required protection ratings, and acceptable fabric codes. Ask for segmented costing (module A, module B, final assembly) so purchase orders match development changes. Force sample gates: prototype, pre-production, and pilot run — no ship without pilot sign-off. Require photos, measurements, and a short video of drop tests for each pilot batch; if suppliers can’t deliver that, they’re not ready. Keep lead-time buffers only where uncertainty exists; shrink them where modules are proven.
Common mistakes and how to avoid them
Don’t accept vague specs like “fits most 15-inch laptops.” Give exact internal width, height, depth. Don’t let MOQ surprises derail planning — lock modules into minimum orders, then scale finished unit runs. Avoid siloed communication: put design, procurement, and the supplier on the same weekly checkpoint with a short agenda. Skip vague QA language; demand pass/fail criteria and an inspection report template you can reuse.
Alternatives to a single-supplier, and quick pros/cons
Option: split modules across specialists. Pro: specialised quality and faster ramp. Con: higher coordination cost and freight. Option: trading company as middleman. Pro: easier communication in your language. Con: less control over factory QA. Option: local prototyping plus Chinese mass production. Pro: fast iteration, then scale. Con: extra handoff risk if specs aren’t frozen. Choose the route that minimises handoffs for critical modules like laptop compartments.
Wrap-up: where value actually sits
Fix the small stuff first — exact compartment specs, moduleised BOMs, and mandatory pilot runs. That problem-driven approach turns late nights and surprise costs into predictable scheduling and buying. For teams that want those predictable outcomes, supply partners who publish module-level traceability and consistent pilot data, such as ChangRong, make planning and purchasing behave like a project rather than a gamble.